


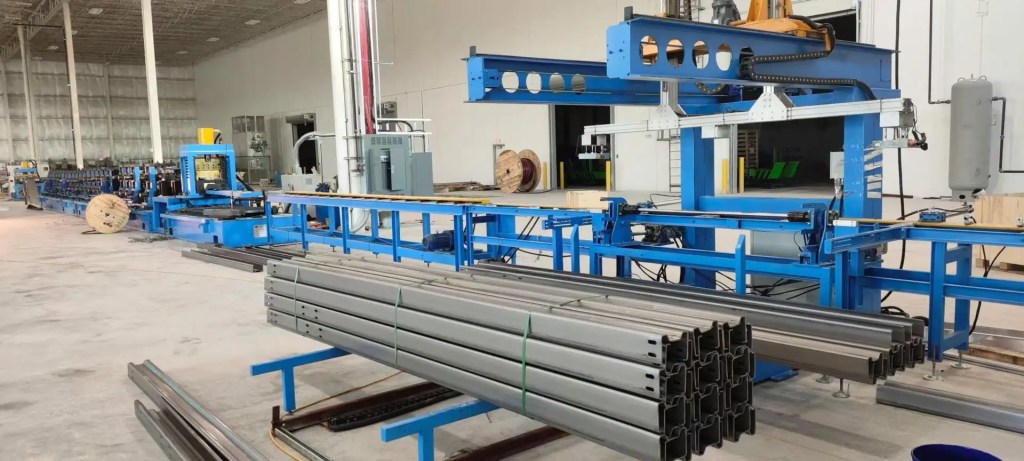
A project buyer in the Kingdom does not shop for a machine. They shop for a profile drawing, a delivery date and a customs file. The line is only useful if it holds tolerance on the section the consultant specified and clears SABER at the port.
Roll forming machine suppliers Saudi Arabia project teams shortlist are judged on four things: the coil range the line can run, tolerance at full speed, the paperwork that ships with it and who stands next to the line during commissioning. Price comes later. A line quoted for 0.8 mm tray stock will not run 2.5 mm purlin stock.
These are the specifications we quote for cable tray and C/Z purlin lines bound for Saudi Arabia, drawn from our own configurations and the standards below. Use them as a first-pass checklist. For the process itself, see our centre de ressources sur le profilage.
1. Pourquoi les spécifications projet déterminent la liste des fournisseurs
Saudi demand is concentrated in industrial buildings, power and water infrastructure, oil and gas facilities and solar plants. Each of those buys a different section. Cable tray goes into electrical containment. C and Z purlins go into the secondary steel of pre-engineered buildings. Both need repeatable hole patterns and tight length control, because they arrive on site as a kit, not as loose stock.
That changes what roll forming machine suppliers Saudi Arabia buyers should be asked. A standard catalogue line is built around one thickness and one width. A project line is built around a range: 1.0-2.5 mm for tray, 1.5-3.0 mm for purlin, and width changes between profile sizes without a tooling swap. Ask for the range in writing, then ask what happens to tolerance at each end of it.
Nos ingénieurs ont configuré des lignes pour des clients dans 50+ pays, notamment les États-Unis, l'Europe et l'Australie, depuis 2005. La version saoudienne de ce travail ajoute trois éléments qui figurent rarement sur un devis standard : la documentation SABER, des armoires électriques résistantes à la chaleur et un kit de pièces de rechange dimensionné pour une chaîne d'approvisionnement longue.
3. Spécifications des lignes de pannes C et Z pour les projets saoudiens
Cable tray sections for Saudi industrial projects are usually perforated or solid bottom tray in galvanized coil. IEC 61537 defines the test method for tray systems, and NEMA VE 1 is the reference many consultants still specify on oil and gas work. Neither standard designs the machine, but both set the load and deflection numbers your finished section has to hit.
| Spec item | Typical project range | What to confirm with the supplier |
|---|---|---|
| Coil material | GI, PPGI, ASTM A653 / EN 10346 | Mill certificate, coating mass, yield strength |
| Épaisseur | 1.0-2.0 mm, up to 2.5 mm heavy tray | Roll gap and drive rating at the thick end |
| Revêtement | Z275, about 275 g/m² total both sides | Compatibility with punching and no white rust |
| Tray width | 50-600 mm automatic, up to 1000 mm | Changeover time, PLC recipe storage |
| Vitesse de la ligne | 10-25 m/min, lower when punching | Speed quoted with or without perforation |
| Forming stands | 12-16 for most tray sections | Stand count for the widest profile |
| Tolérance de longueur | ±1.0 mm over 6 m | Cutoff type and encoder feedback |
| Perforation | Servo or hydraulic prepunch | Hole pitch, burr limit, die life |
Perforation is the usual bottleneck. A line quoted at 25 m/min may only hold that on unperforated tray. Ask for the speed with the actual hole pattern running, and ask for a sample cut from that test. The difference between a servo punch and a hydraulic prepunch is covered in our cable tray machine buying guide.
If the project mixes tray and ladder sections, confirm the rung welding or riveting station before you sign. The two sections are not the same product, and the difference is explained in our cable tray vs cable ladder comparison.

3. C/Z Purlin Line Specs for Saudi Projects
A purlin line has to do something a tray line does not: switch section shape and web height while keeping hole positions aligned. On pre-engineered buildings, the purlin holes carry the bracing and the cladding fixings. A 2 mm drift at the punch station shows up as a fit problem on site, hundreds of metres away from the machine.
| Spec item | Typical project range | What to confirm with the supplier |
|---|---|---|
| Sections | C, Z and Sigma from one line | Manual or automatic C to Z changeover |
| Épaisseur | 1,5-3,0 mm | Drive power at 3.0 mm, not just 1.5 mm |
| limite d'élasticité | 250-350 MPa, S350GD or equivalent | Roll material and shaft diameter |
| Web height | 100-300 mm adjustable | Spacer stack or servo adjustment |
| Vitesse de la ligne | 10-20 m/min with punching | Speed at maximum web height |
| Perforation | Web and flange holes, servo feed | Hole position tolerance across a batch |
| Tolérance de longueur | ±1.0 mm over 6 m | Flying shear or stop shear |
| Empiler | Automatic stacker, 6-12 m lengths | Stacker length and bundling method |
AISI S100 sets the design basis for cold-formed steel members in many international projects, and it is the reference most structural consultants will quote back to you. The machine does not certify the member, but it has to produce the section the calculation assumes. Ask the supplier for a measured section report, not a drawing. Our Guide d'achat des pannes en Z et comparaison pannes C vs Z explain how the changeover works.
4. Conformité, normes et conditions du site
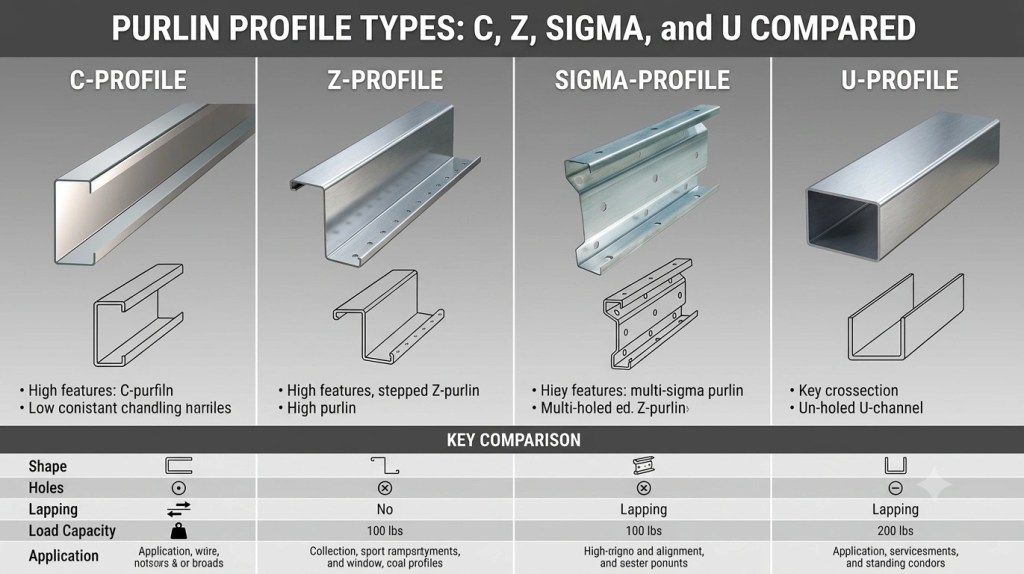
Import paperwork is a specification, not an afterthought. A machine entering the Kingdom needs a SABER product registration and a SASO conformity certificate before customs release. Our six step SASO guide covers the HS code, technical regulation and factory audit sequence. Ask any supplier on your shortlist who prepares that file. If the answer is “the buyer handles it”, the machine may sit at the port.
Site conditions matter as much as the paperwork. Summer ambient temperatures above 45 °C and airborne dust push electrical cabinets toward IP54 or better, with cabinet cooling specified separately. Hydraulic oil viscosity, sensor sealing and PLC cabinet ventilation should be listed on the offer. The Fabricator has covered how heat and contamination affect roll forming uptime in plant conditions.
Standards worth naming in the technical offer: ASTM A653 for galvanized sheet, EN 10346 for continuously hot dip coated steel, IEC 61537 and NEMA VE 1 for cable tray systems, AISI S100 for cold-formed steel design, and SASO for the conformity route. ISO 9001 and CE documentation should travel with the machine, not follow it by email three weeks later.
5. Comment comparer les fournisseurs de profileuses en Arabie saoudite
Most supplier comparisons stop at price and delivery. On project work, the differences that cost money appear after installation. Use this checklist on every offer, including ours.
| Checkpoint | Ask for | Pourquoi est-ce important ? |
|---|---|---|
| Profile confirmation | Signed profile drawing and tolerance sheet | Fixes the tooling design before steel is cut |
| Coil range | Written min and max thickness and yield | Prevents a line that only runs one gauge |
| Speed basis | Speed with punching and cutoff active | Catalogue speed is often unperforated speed |
| Automation scope | Decoiler, leveler, punch, shear, stacker list | Missing stations become hidden site costs |
| Controls | PLC brand, drive brand, recipe storage | Determines spare parts and local support |
| Compliance file | SABER, SASO CoC, CE, ISO 9001, MTC | Determines customs release and site acceptance |
| N/A (pas un fournisseur de machines) | Named engineer, days on site, training hours | Startup quality sets first year output |
| Des pièces de rechange | Two year wear kit with prices | Protects the delivery schedule |
Roll forming machine suppliers Saudi Arabia projects can rely on will answer all eight in writing. A quotation that only lists “complete line” and a total price is not a technical offer. For a second category example of how we specify punching and model ranges, see our Guide d'utilisation d'une machine à profilés en U pour l'Arabie saoudite.
6. Livraison, mise en service et pièces de rechange
Standard cable tray and purlin lines ship in 45-60 days from drawing approval. Custom punching or a second profile set adds time. Lock that into the schedule before the order.
A commissioning plan names the engineer, days on site, training hours and the acceptance test. That test should run your project coil at production speed with the real hole pattern, then measure length, hole position and section dimensions. Anything less proves the machine turns on, not that it makes your section.
Ask for a two year wear kit priced with the line: punches, dies, shear blades, sensors, hydraulic seals and drive belts. On a long supply chain, a cheap seal can idle a whole line. We ship a labelled parts list with the kit so the local team can reorder without a drawing exchange.
Questions fréquentes
1. Qui sont les fournisseurs de profileuses pour les projets en Arabie saoudite ? Three groups: local distributors, regional trading houses and direct manufacturers like Beli Rollforming. Direct manufacturers handle profile design and tooling in house, which matters when a consultant changes a section.
2. Quelle épaisseur une ligne saoudienne de chemins de câbles doit-elle couvrir ? Specify 1.0-2.0 mm as the working range, and 2.5 mm if the project includes heavy tray.
3. Une seule ligne peut-elle produire chemins de câbles et pannes C/Z ? Not on the same tooling. Tray and purlin need different roll sets, punch dies and cutoff blades, though a decoiler, leveler and PLC can be shared.
4. La machine elle-même nécessite-t-elle un certificat SASO ? Yes. The machine needs SABER product registration and a SASO conformity certificate before Saudi customs release.
5. Quelle vitesse de ligne inscrire dans le cahier des charges ? Write 10-25 m/min with the qualification “with punching and cutoff active”.
6. Quel revêtement spécifier pour les chemins de câbles en Arabie saoudite ? Z275 hot dip galvanizing, about 275 g/m² total both sides, under ASTM A653 or EN 10346.
7. Quelle tolérance de longueur est réaliste sur les pannes ? ±1.0 mm over a 6 m length with encoder feedback and a servo cutoff.
8. Faut-il des armoires électriques avec indice IP en Arabie saoudite ? Yes for most sites. Ambient heat above 45 °C plus dust calls for IP54 or better with separate cabinet cooling.
9. Quel est le délai de livraison ? Standard lines ship in 45-60 days from drawing approval.
10. Que doit contenir un forfait de mise en service ? A named engineer, defined days on site, training hours and an acceptance test on your own coil at production speed.
Conclusion
Roll forming machine suppliers Saudi Arabia buyers select should be able to put eight numbers on paper before a price: thickness range, yield strength, width range, speed with punching, stand count, length tolerance, coating mass and cabinet rating. Add the SABER and SASO file, and the comparison becomes objective.
Send us your profile drawing, steel grade and target output. Our engineers reply within 24 hours with a configured line, a lead time and a price. Demander un devis or email enquiry@belirollforming.com.
Dernière mise à jour : 2026-11-09
Journal des modifications de l'article
- 2026-11-09: Initial publication. Added cable tray and C/Z purlin project spec tables, Saudi compliance checklist, supplier comparison table and 10 FAQ.
Déclencheurs de la prochaine révision
- SASO or SABER technical regulation changes for machinery imports.
- GSC or AI citation movement on “roll forming machine suppliers for Saudi Arabia market”.
- New project requirement outside 1.0-3.0 mm coil thickness or 1000 mm width.
- Quarterly refresh of lead time, cabinet rating and commissioning scope.



 Français