


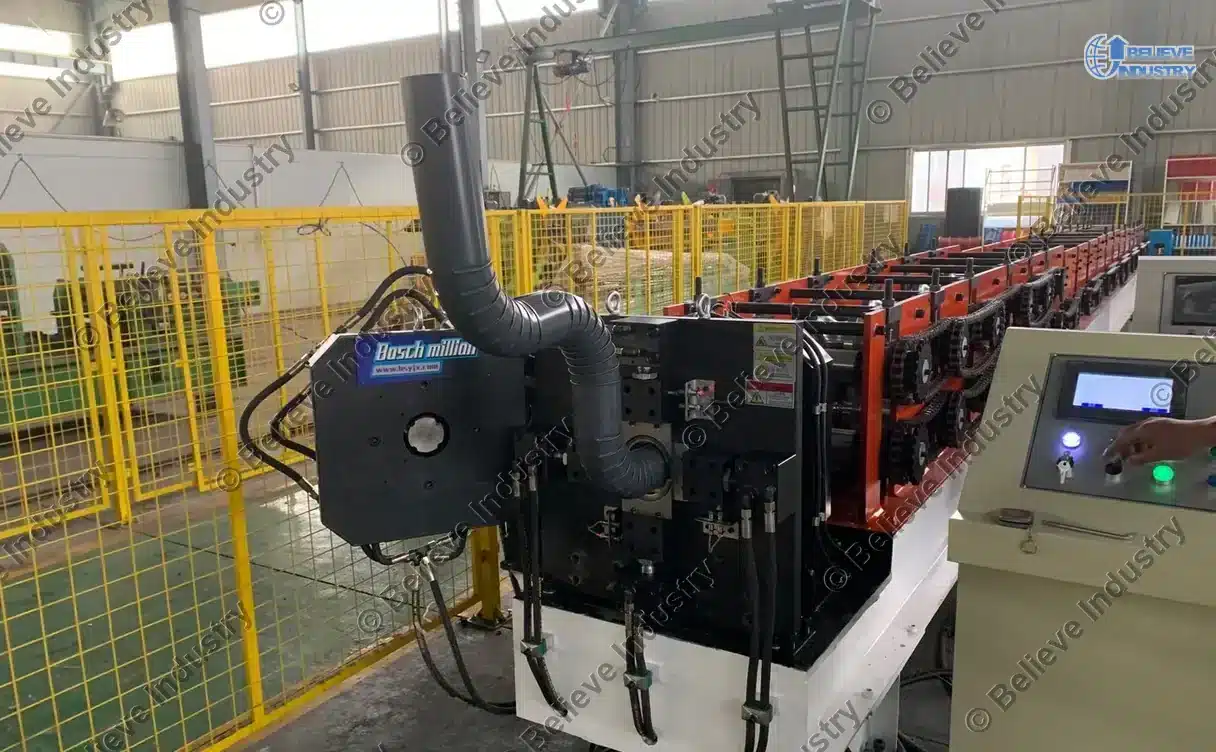

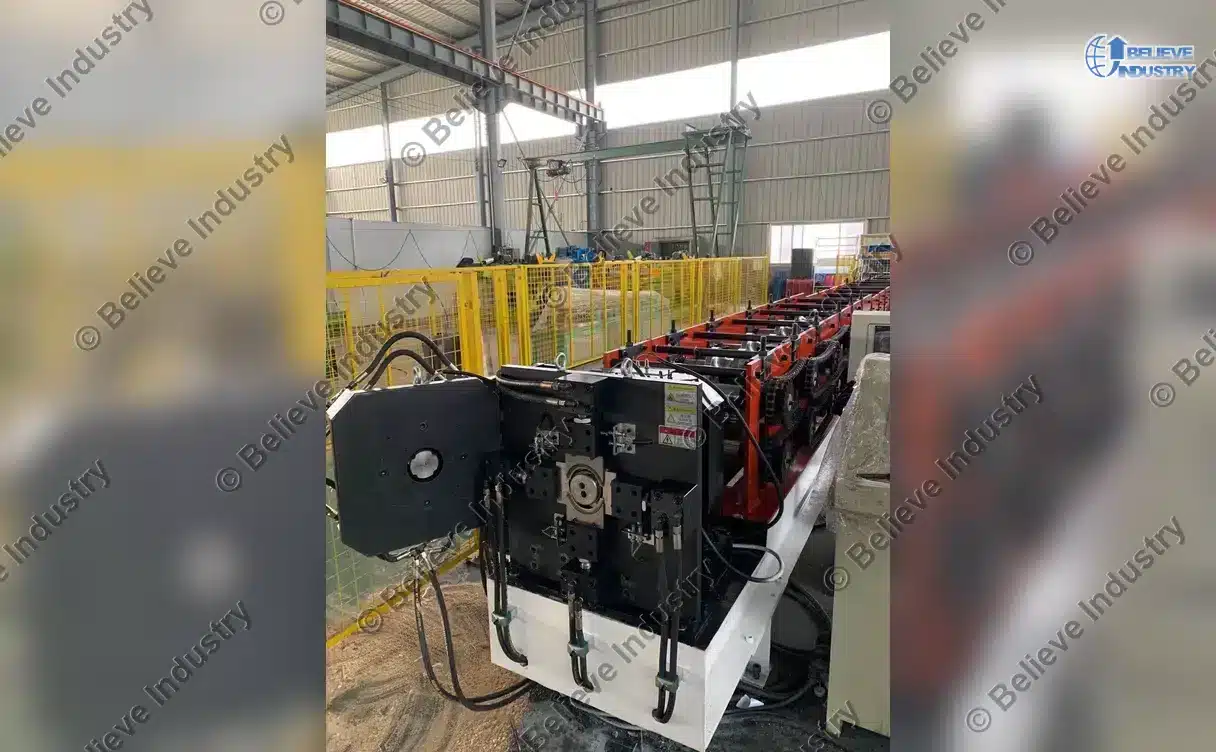
A downspout roll forming machine turns coated steel coil into a finished rainwater downpipe in one continuous line. Coil goes in at one end. A formed, seamed and cut-to-length pipe comes out at the other. The same downspout roll forming machine can also make elbows and shrunk ends, either on the line or at a separate station.
Buyers use two names for this product. Downpipe roll forming machine is common in the UK, Australia and the Middle East. Downspout roll forming machine is common in North America. They describe the same downspout roll forming machine. We build both round downpipes and rectangular downspouts in the same machine family.
Beli Rollforming has made custom roll forming machines since 2005. We have delivered 500+ machines to 50+ countries from a 15,000 m² factory. Each downspout roll forming machine is laid out around the profile drawing you send, not around a catalogue model.
Round downpipes and rectangular downspouts
A round downpipe is the classic rainwater pipe from a downspout roll forming machine. The strip folds into a closed circle and the seam sits at the top of the section where the fixings hide it. Sizes in our current drawing set run from Round 80 to Round 130. The round shape drains well and needs the fewest forming passes.
A rectangular downspout gives a flat face to the wall and a sharper look on modern buildings. It is also easier to pack and to fix to a bracket. Our rectangular drawings include the LSG 125×100 section and the YX75-101 section. Both carry shallow ribs along the flat faces. The ribs stiffen a thin wall without adding thickness.
Octagonal sections sit between the two. The Octagon 400 drawing shows a ribbed corner profile. It gives the stiffness of a shaped section with the water capacity of a round pipe. All three shapes run on one downspout roll forming machine with a tooling change. All eight sections below close with a small overlap at the top of the profile.
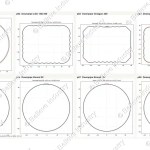
The table lists the eight sections in the current CAD set. Designation is the drawing name in that set. Final dimensions, coil width and pass count are fixed by your own profile drawing.
| Drawing | Forma | Designation | Espessura da tira |
|---|---|---|---|
| p01 | Round | Downpipe Round 130 | 0,5 mm |
| p02 | Retangular | Downpipe LSG 125×100 | 0,6 mm |
| p03 | Octagonal | Downpipe Octagon 400 | 0,5 mm |
| p04 | Retangular | Downpipe YX75-101 | 0.8 mm |
| p05 | Round | Downpipe Round 88 | 0,5 mm |
| p06 | Round | Downpipe Round 92 | 0,5 mm |
| p07 | Round | Downpipe Round 100 | 0,5 mm |
| p08 | Round | Downpipe Round 80 | 0,5 mm |
Five round sizes, two rectangular sections and one octagonal section are in this set. Strip thickness runs from 0.5 to 0.8 mm. A downpipe roll forming machine for a new market usually starts from one of these drawings and then changes to the local size.
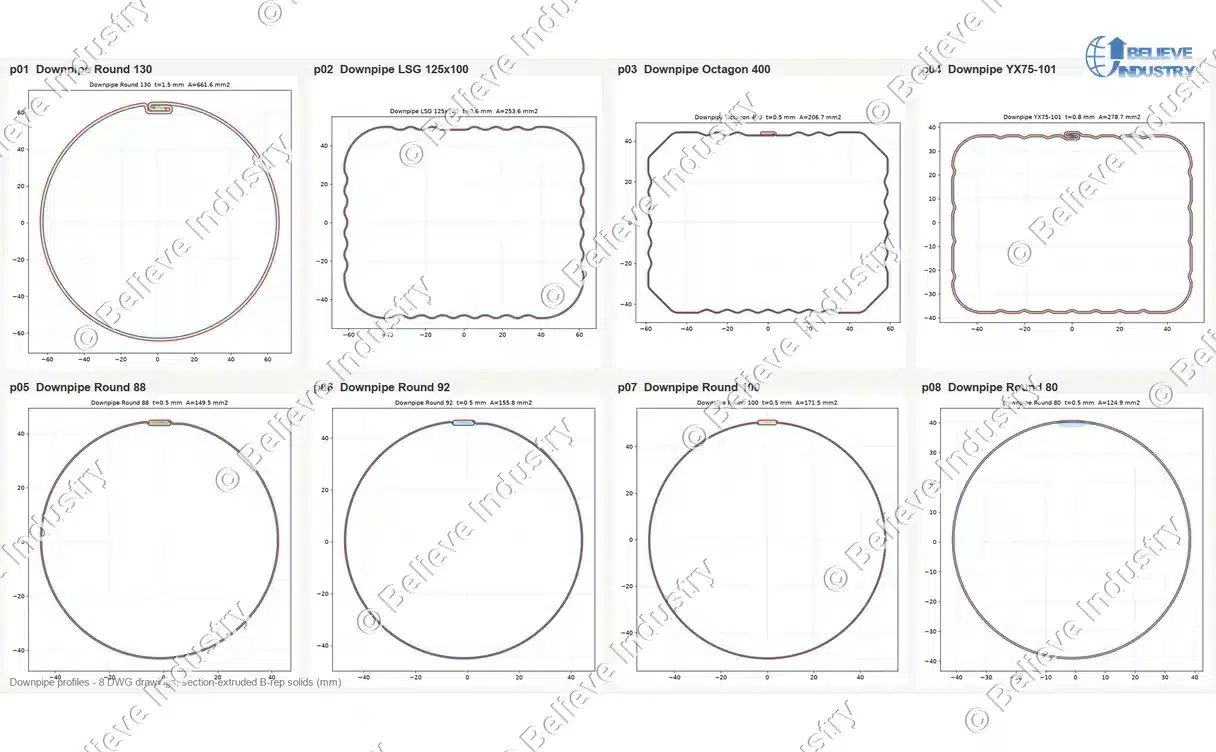
Eight downpipe sections drawn for this downspout roll forming machine family. Five round, two rectangular and one octagonal. STEP and DXF files for each section are available on request.
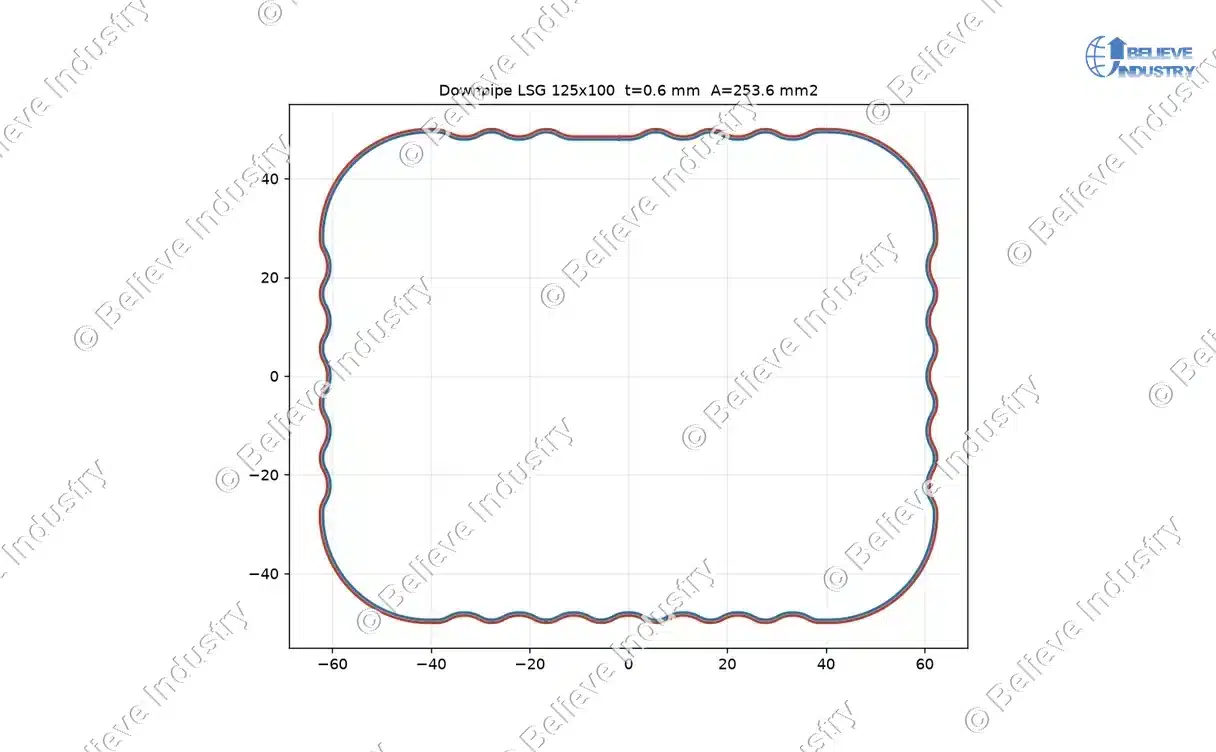
The LSG 125×100 rectangular downspout section. The ribbed flat walls and rounded corners are formed in the same pass sequence as the round pipes.
Getting from a section drawing to a stable pipe on a downspout roll forming machine is a roll pass design problem. The flower pattern, stand spacing and seam closing rolls all come from the profile, not from the machine size. Our engineering notes set out that sequence step by step.
Como se projeta uma máquina de perfilagem a frio
Inline elbow or offline elbow
An elbow joins the downpipe to the gutter outlet or turns the pipe around an eave. You can make it on the downspout roll forming machine or on a separate machine. The choice changes labour, floor space and how fast you can change a size.
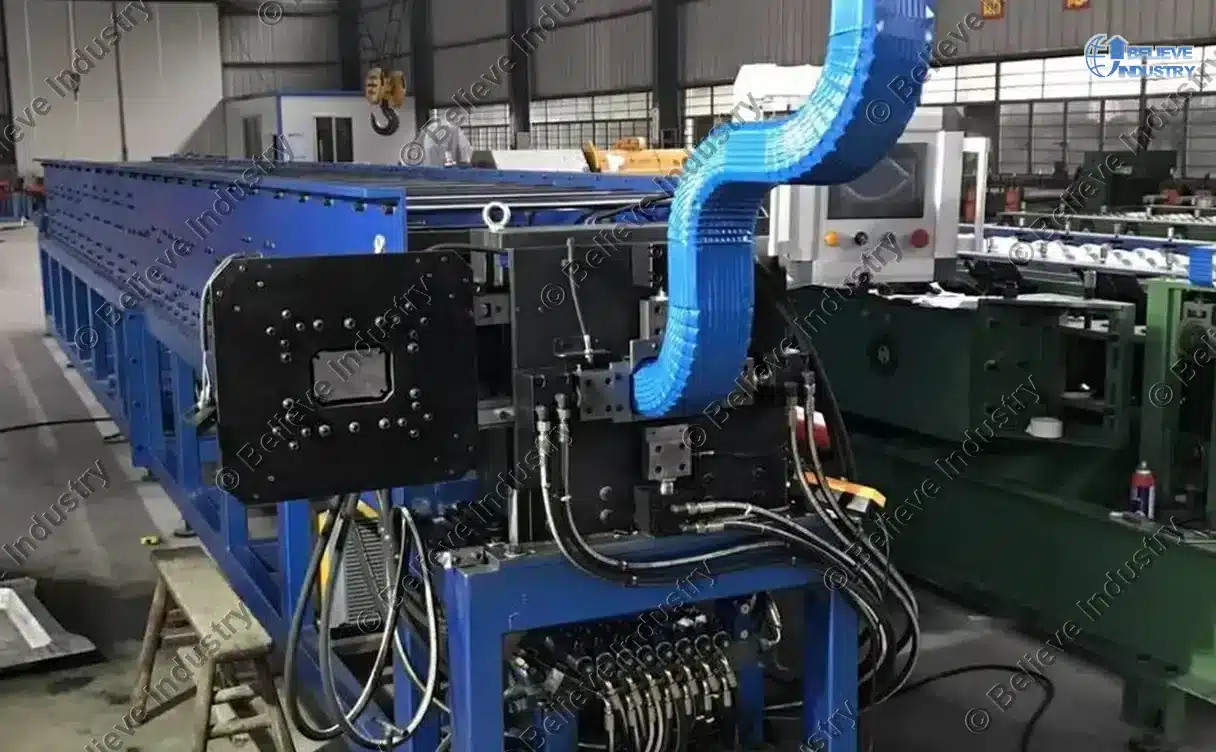
With an inline elbow station, the formed pipe runs through a bending head before the flying cut. One operator runs the whole downspout roll forming machine. The elbow angle and bend radius come from the tooling set. This suits long runs of one angle, usually 45, 60, 75 or 90 degrees. An inline elbow on a downspout roll forming machine removes a whole handling step.
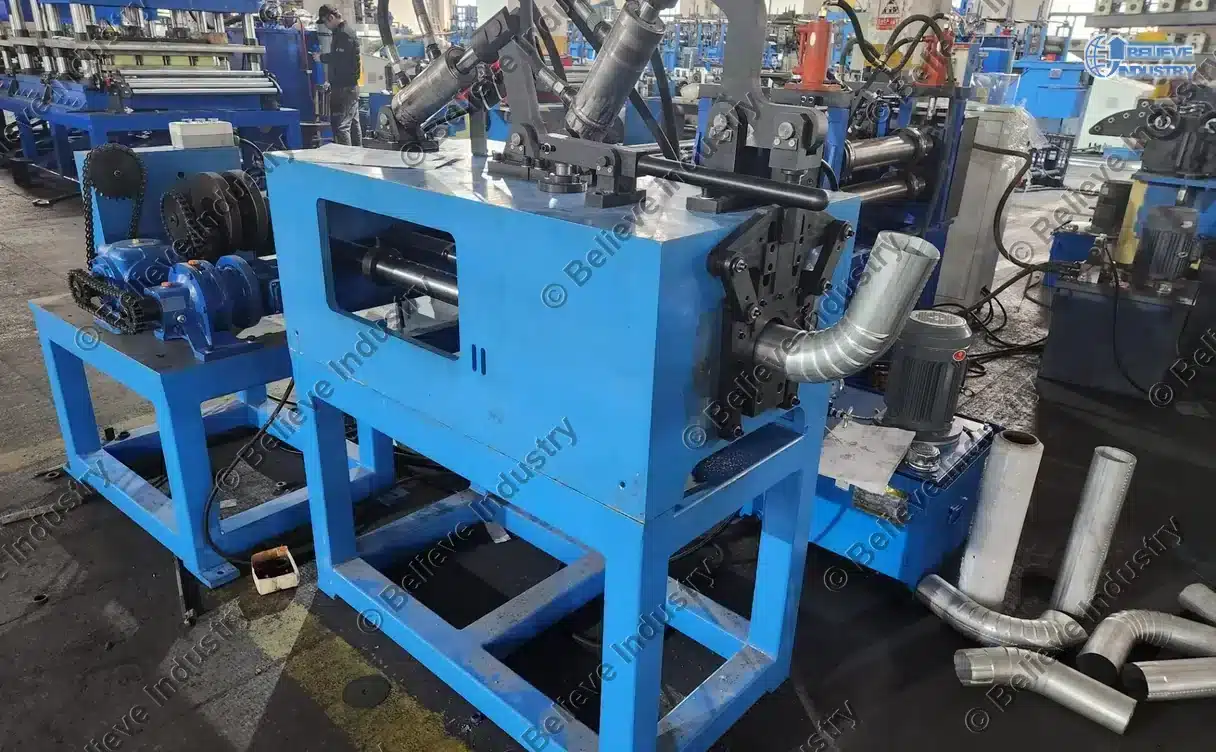
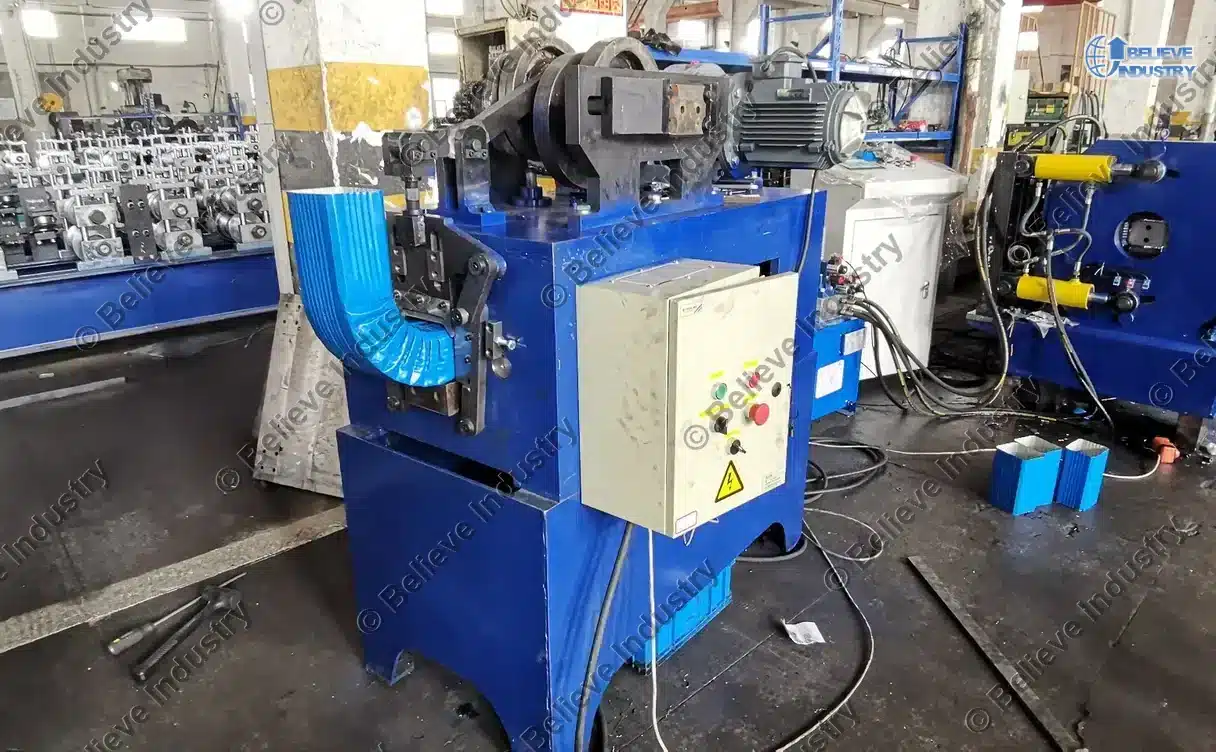
With an offline elbow machine, straight pipes leave the downspout roll forming machine and go to a separate bending cell. One downspout roll forming machine can feed two or three elbow machines. You gain freedom on angle, radius and batch size. You also add one operator and one handling step. Job shops that serve many roof designs usually pick this route.
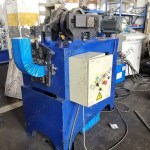
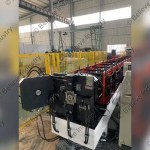
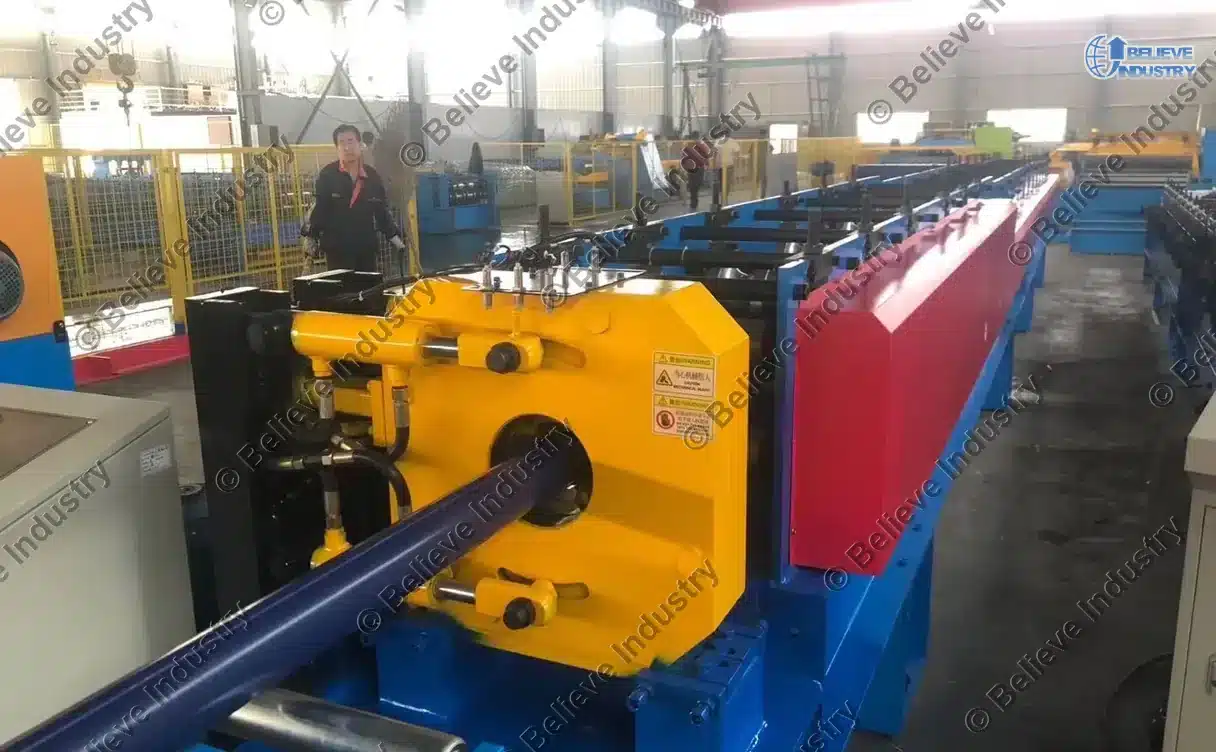
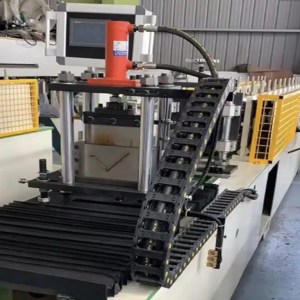
The photographs below show both routes for round downpipes and for rectangular downspouts. The ribbed blue and black samples are elbows made on the machine behind them, not bought-in fittings.
Inline shrinking or offline shrinking
A shrunk end, sometimes called a swaged end, is a short reduced diameter at one end of the pipe. One pipe then slides into the next one. Installers use fewer separate couplings and the joint sheds water.
On an inline shrinking station of a downspout roll forming machine, a hydraulic die forms the reduced end before the cut. Timing comes from the same line encoder as the shear. The pipe leaves the line ready to install. This is the usual choice when a downpipe roll forming machine runs one diameter for a full shift.
On an offline shrinking machine, cut pipes are fed one at a time into a standalone press. One press can serve several pipe sizes with a die change. It is slower per piece, but it keeps the downspout roll forming machine simple and lets you shrink only the batches that need it.
Elbow and shrinking choices are independent. Four configurations cover most plants.
| Configuração | Elbow station | Shrunk end station | Uso típico |
|---|---|---|---|
| 1 | Em linha | Em linha | One pipe size, long runs, one operator, finished parts off the line |
| 2 | Em linha | Offline | Fixed elbow angle, several pipe diameters sharing one shrinking press |
| 3 | Offline | Em linha | Many elbow angles, one pipe diameter, coupling-free installation |
| 4 | Offline | Offline | Job shop work, many profiles, small batches, frequent size changes |
Configuration 1 puts the most work on the downspout roll forming machine and gives the lowest labour per part. Configuration 4 keeps the most flexibility. Output planning has to start from the real cycle time of the elbow and shrinking stations, not from the top speed on the nameplate.
Planejamento da produção em perfilagem a frio de alto volume
Profile drawings and 3D models
Every downpipe roll forming machine starts with a section drawing and a 3D model of the finished pipe. Our engineers use the model on every downspout roll forming machine to check the seam position, the rib depth and the corner radii before any roller is cut. It also shows the buyer what the pipe will look like on the wall.
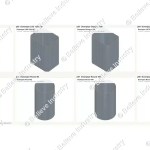
The eight models below match the eight section drawings above. Each one is a short extruded segment. We supply STEP and DXF files for the section, along with the roll pass flower pattern, after the order is confirmed. Profile drawings are kept in the machine file so replacement rolls can be made years later.
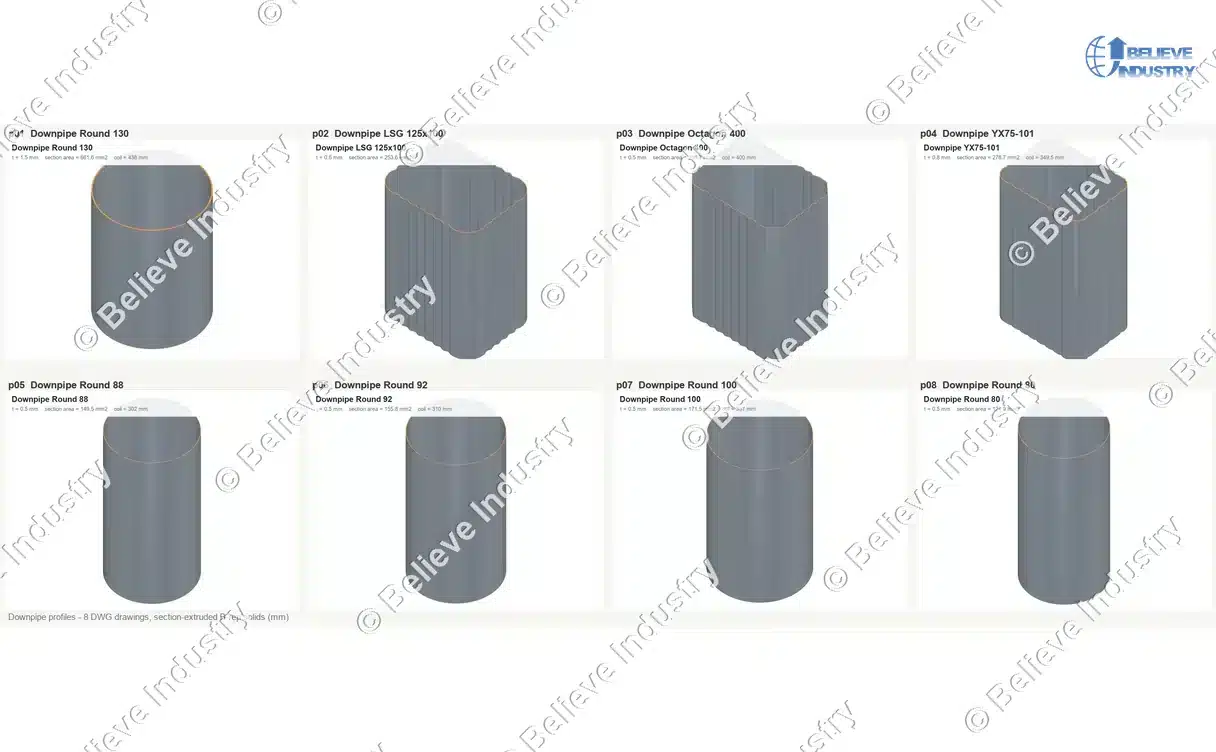
Eight 3D models from the same drawing set. Round pipes, ribbed rectangular downspouts and the octagonal section are all formed from flat coil.
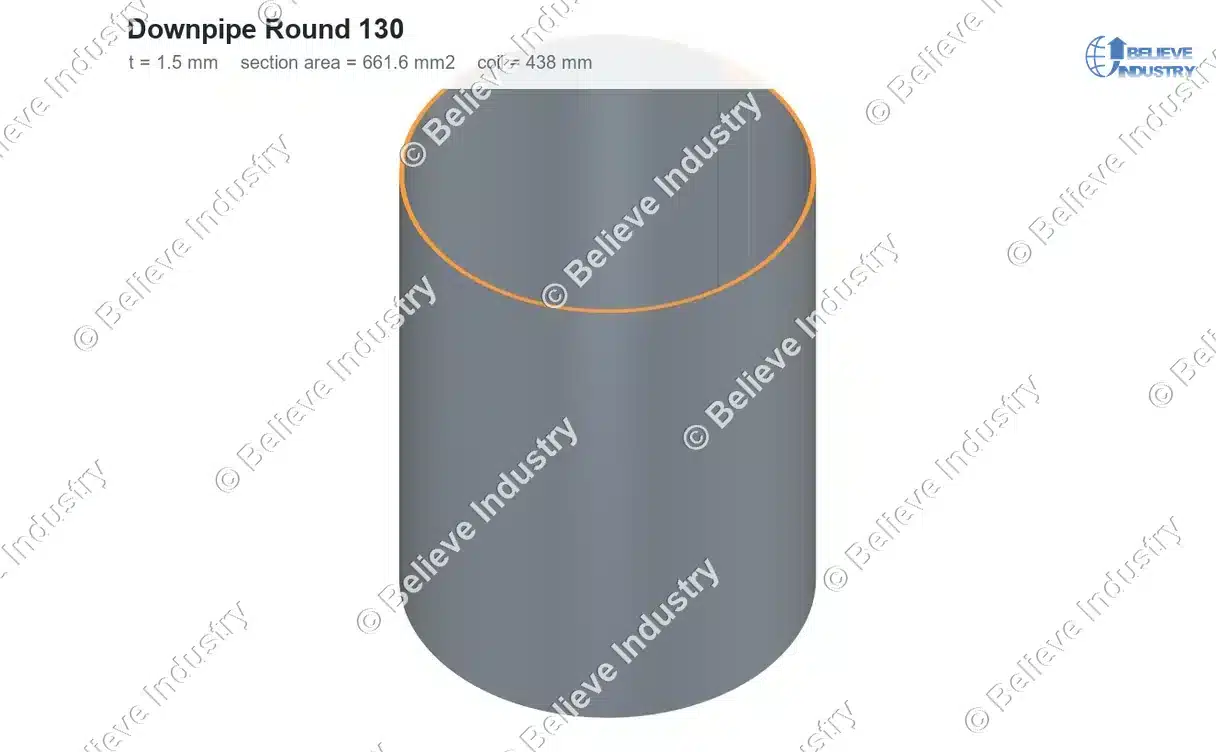
Round 130 model. The seam overlap sits at the top of the section where the bracket covers it.
A downpipe made on a downspout roll forming machine is only one part of a rainwater system. The gutter that feeds it sets the outlet size, the bracket spacing and the elbow angle. Buyers who order both machines usually get a matched outlet drawing with the line.
Como a linha funciona, estação por estação
The strip does not stop between the stations. A downspout roll forming machine takes its timing from one line encoder, so the feed, the seam rolls, the bending head and the flying shear stay in phase.
- Hydraulic uncoiler pays out the coated coil under controlled tension.
- A leveler flattens the strip before the first forming pass.
- The roll forming mill folds the strip through a flower pattern set by your section drawing.
- Seam closing rolls lock the overlap at the top of the pipe.
- The elbow station bends the pipe inline, or the straight pipe leaves the line for an offline elbow machine.
- The shrinking station reduces one end inline, or cut pipes go to an offline shrinking press.
- A servo tracking flying shear cuts to the programmed length.
- An outfeed table collects the finished pipes.
A rectangular downspout on a downspout roll forming machine needs more passes than a round pipe of the same wall thickness because the corners and the ribs have to hold their shape. The PLC stores a recipe for each section, so a downpipe roll forming machine with two tooling sets can run two profiles on the same mill.
Parâmetros técnicos
The ranges below describe the downspout roll forming machine family on this page. They are not a fixed quotation. Your profile drawing, coil specification and target output set the final pass count, line speed and tooling list.
| Item | Range or option | Fixed by |
|---|---|---|
| Material | Galvanized steel, prepainted steel, aluminum, copper | Your coil specification |
| Espessura da tira | 0.5 to 0.8 mm in the current drawing set | Profile drawing |
| Sections | 5 round, 2 rectangular, 1 octagonal | Profile drawing |
| Round designations | Round 80, 88, 92, 100, 130 | Profile drawing |
| Rectangular designations | LSG 125×100, YX75-101 | Profile drawing |
| Seam | Lock seam or snap seam at the top of the section | Profile drawing and local practice |
| Elbow | Inline bending head or offline elbow machine | Product mix and floor space |
| Shrunk end | Inline hydraulic die or offline shrinking press | Product mix and batch size |
| Passes de conformação | Set by the flower pattern of the section | Profile drawing |
| Corte | Servo tracking flying shear | Cut length list |
| Controlar | PLC, touch screen HMI, line encoder, recipe per section | Plant standard |
| Fonte de alimentação | Matched to your plant supply | Plant standard |
| Garantia | 24 meses para a máquina completa | Beli Rollforming standard |
Materials and standards
Finished downpipes from a downspout roll forming machine are checked against your drawing and against the standard used in your market. EN 612 covers metal eaves gutters and downpipes. ASTM A653 and ASTM A792 cover hot dip galvanized and aluminum-zinc coated steel sheet. ASTM B370 covers copper sheet for rainware. EN 10346 covers continuously hot dip coated flat products. GB/T 6725-2008 covers cold formed steel sections. We list the organisations below so your engineers can verify a material or a joint detail before it reaches a purchase order.
The Metal Construction Association publishes guidance on metal roofing and rainwater systems for North American projects.
Metal Construction Association on metal rainwater systems
Copper Development Association material data applies when the downpipe is copper rather than coated steel.
Copper Development Association on copper rainware
The American Galvanizers Association explains zinc coating life and outdoor corrosion for galvanized parts.
American Galvanizers Association on zinc coatings
The Aluminum Association publishes alloy and finishing data for painted aluminum downpipes.
Aluminum Association on aluminum sheet alloys
SMACNA sheet metal manuals cover the seam and joint practice used on rectangular downspouts.
Roof edge trims are often ordered with the rainwater package. They use the same coated coil and the same folding logic on a smaller mill.
Supplier comparison
Buyers usually compare three things before they sign: who designs the roll passes, who makes the elbow and shrinking tooling, and who fixes the line when it stops. Here is how our downspout roll forming machine differs.
| Point | Beli Rollforming | Typical low cost line | Typical EU or US line |
|---|---|---|---|
| Projeto dos passes de conformação | In house from your CAD section | Often reused from an existing section | Interno, com prazo de engenharia maior |
| Section drawings | DXF and STEP supplied with the machine | Drawings often not supplied | Supplied at extra cost |
| Elbow option | Inline head or offline cell, as ordered | Usually a separate manual bender | Geralmente uma célula separada |
| Shrunk end option | Inline die or offline press, as ordered | Often omitted | Disponível a um custo maior |
| Seam closing | Tooling matched to the section | Hand finished at the exit | Automated at extra cost |
| Garantia | 24 meses para a máquina completa | Varia conforme o fornecedor | Varia conforme o fornecedor |
| Comissionamento | Nossos engenheiros processam as primeiras bobinas no local | Frequentemente apenas suporte remoto | No local, com custo adicional |
We do not claim to be the cheapest line on a quotation sheet. We build for plants that run the same pipe every day and cannot afford a seam that opens after six months.
Fascia gutters are the other half of a matched eaves system. Sizing the gutter outlet and the downpipe together avoids a step that leaks at the first heavy rain.
Why choose Beli for your downpipe line
Fabricamos máquinas de perfilagem a frio sob medida desde 2005. Entregamos 500+ máquinas para 50+ países a partir de uma fábrica de 15,000 m², com 80+ engenheiros e técnicos na equipe.
Every downpipe roll forming machine ships with a 24-month warranty on the complete machine. Wear parts and consumables are excluded. That covers the mechanical, hydraulic and electrical systems as one package.
Our engineers install and commission the downspout roll forming machine at your plant. They run the first coils with your operators and hand over only when the pipe holds the tolerances in your drawing. You get the section drawings, the roll pass flower pattern, the tooling list and the QC records with the machine.
Send us the profile drawing, material grade, thickness, elbow angle and target output. We reply within 24 hours with a line layout, a tooling list and a quotation for a downspout roll forming machine built to that drawing.
Perguntas frequentes
A downspout roll forming machine is a continuous line that turns coated steel coil into a finished rainwater downpipe. The line uncoils, levels, roll forms, closes the seam, makes the elbow and shrunk end if ordered, and cuts to length in one pass. Round and rectangular sections run on the same machine family with a different roll tooling set.
Yes. Downpipe is the common term in the UK, Australia and the Middle East. Downspout is the common term in North America. Both names describe the same roll forming line. We use both on this page so buyers find the machine under either name.
Yes. A downspout roll forming machine uses a separate roll tooling set and a stored PLC recipe for each section. The mill, uncoiler, seam rolls and shear stay the same. The current drawing set covers five round sizes, two rectangular sections and one octagonal section.
An inline elbow station on a downspout roll forming machine bends the formed pipe before the flying cut. One operator runs the whole machine and no handling step is added. The angle comes from the tooling, so it suits long runs of a fixed angle such as 45, 60, 75 or 90 degrees.
Choose an offline elbow machine with your downspout roll forming machine when you serve many roof designs, need several angles and radii, or change size often. One forming line can feed two or three bending cells. You add one operator and one handling step, but you gain batch flexibility.
A shrunk end, also called a swaged end, is a short reduced diameter at one end of the pipe. One pipe slides into the next one. Installers need fewer separate couplings and the joint sheds water.
Yes. On a downspout roll forming machine, a hydraulic die forms the reduced end before the cut and takes its timing from the line encoder. The pipe leaves the line ready to install. An offline shrinking press is the alternative when several diameters share one press.
A downspout roll forming machine runs galvanized steel, prepainted steel, aluminum and copper coil. The current drawing set uses 0.5 to 0.8 mm strip. Coated steel is the usual choice for volume work. Copper and aluminum need a different roll finish and seam detail, which we set from your coil specification.
EN 612 covers metal eaves gutters and downpipes. ASTM A653 and ASTM A792 cover coated steel sheet, and ASTM B370 covers copper sheet. EN 10346 covers hot dip coated flat products and GB/T 6725-2008 covers cold formed steel sections. We check the pipe against your drawing and the standard used in your market.
Send the profile drawing, material grade, strip thickness, elbow angle, shrunk end requirement and target output. We reply within 24 hours with a line layout, a tooling list and a quotation. Every machine ships with a 24-month warranty on the complete machine.
Get a quote for your downspout roll forming machine
Send us your downpipe section drawing. We respond within 24 hours with a complete quotation for a downspout roll forming machine:
- A line configuration matched to your profile, material and output target
- A layout drawing with the elbow and shrinking stations in the order you choose
- A roll tooling list, a die list and the section drawings in DXF and STEP
- Um cronograma estimado de entrega e comissionamento
Envie seu desenho e receba uma cotação hoje
Se você ainda está comparando fornecedores, nosso guia do comprador apresenta as perguntas a fazer sobre projeto dos passes de conformação, rolos sobressalentes, comissionamento e condições de garantia antes de assinar um contrato.
Última atualização: 12 de novembro de 2026
Histórico de alterações do artigo
November 12, 2026. Initial publication. Eight section drawings and eight 3D models added from the downpipe CAD set. Workshop photographs of inline and offline elbow machines, shrinking heads and complete lines added.
Gatilhos para a próxima revisão
Review when a new profile drawing is added to the CAD set, when a new elbow or shrinking station is built, or when the strip thickness range changes. Review when profile drawings and 3D models are replaced by a new revision.

 Português
Avaliações
Ainda não existem avaliações.