

مقدمة
Roll forming surface scratch defects are the most common quality rejection on a cold forming line. A single deep scratch can send a whole panel to scrap. With 20 to 40 percent of defects in rolled products traced to surface damage, the cost adds up fast.
Most scratches are not random. They come from two repeatable sources: roller surface condition and roller gap settings. Fix both and most mark defects disappear.
This guide covers six roller polish and gap solutions for خدش على سطح الشريط المشكل بالدرفلة control. You get roller gap starting values, target finishes, and a maintenance schedule that stops scratches before they start.
Roll forming surface scratch problems are best solved at the أدوات تشكيل اللفائف level. For the full machine picture, see the مكونات آلة تشكيل اللفائف مرشد.
What Are Roll Forming Surface Scratch and Mark Defects?
A surface defect is any unintended scratch, mark, or blemish left on the strip after it passes through the forming stands. Roll forming surface scratch defects are grooves, lines, or gouges aligned with the strip travel direction. Mark defects are shorter, wider, and shaped like the roller or debris that caused them.
Three defect families cover almost every case:
- Scratches: continuous lines along the profile, caused by roll surface roughness, embedded debris, or a too-tight فجوة الأسطوانة.
- Marks: localized dents, pressure marks, or transfer marks, caused by coating pick-up, hard particles, or misaligned stands.
- Galling: heavy metal-to-metal transfer where the strip welds onto the roll surface and tears on every pass.
Each family needs a different fix. A فحص تشكيل اللفة routine catches all three early, before they hit the finished profile.
Why Roll Forming Surface Scratch Defects Form
Scratches form when a hard surface slides against the strip under pressure. The roll face is harder than the material, so the material loses the fight, a pattern documented by المُصنِّع.
Four root causes drive nearly all surface damage:
- Rough or damaged roll surfaces. Worn rollers, grinding marks, or corrosion on the roll face act like sandpaper on the strip.
- Roller gap set too tight. When the gap is smaller than actual material thickness, the rolls squeeze, thin, and scuff the surface.
- Coating pick-up. Zinc, paint, or oxide builds up on the roll face and transfers as repeating marks.
- Contaminated strip. Dust, scale, or metal fines between the strip and roll act as abrasive particles.
Most lines show all four at once, which is why fixing one cause alone never clears the defect.
The 6 Roller Polish and Gap Solutions
Solution 1: Polish Rolls to the Correct Surface Finish
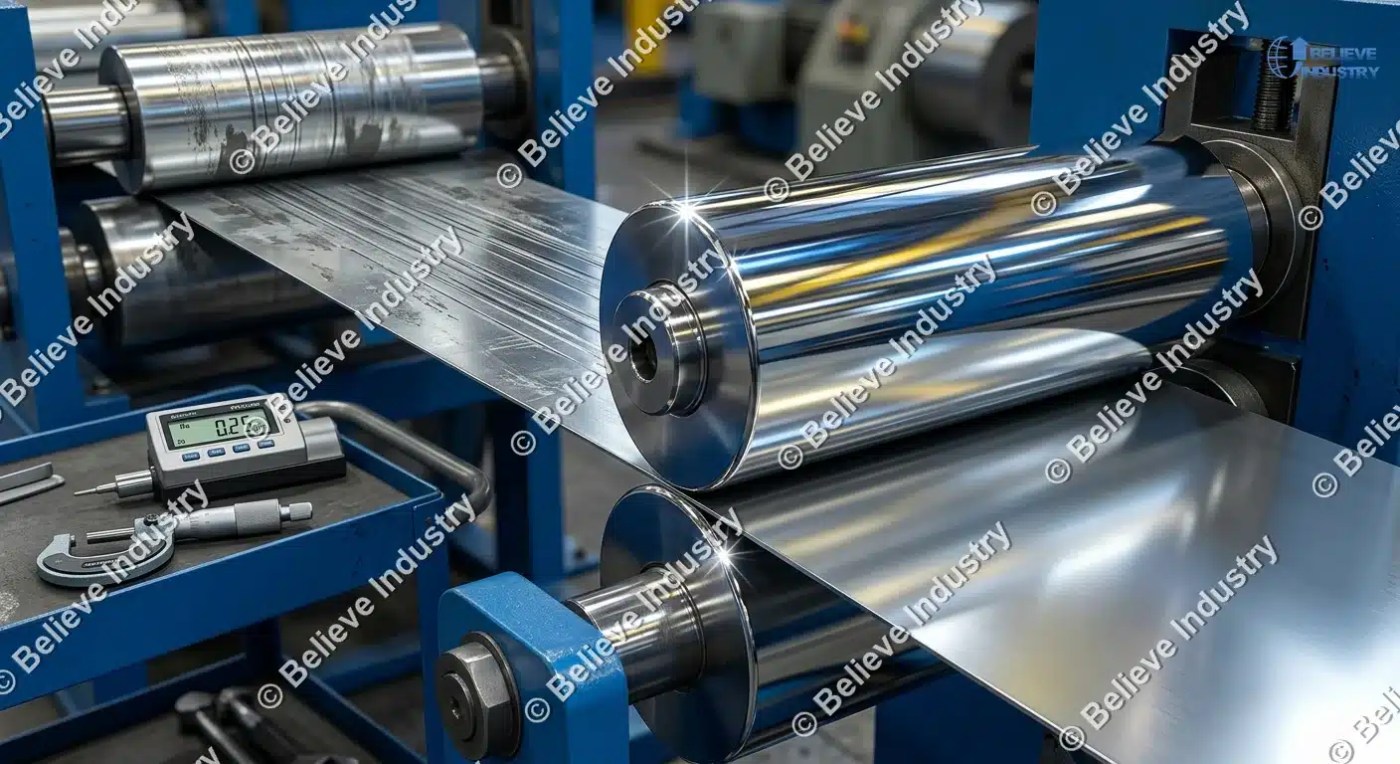
Roller polish quality is the single biggest factor in خدش على سطح الشريط المشكل بالدرفلة control. A rough roll face imprints its texture into every meter of strip.
Target an Ra of 0.2 to 0.4 micrometers for forming rolls that touch exposed surfaces. Finish idle and guide rolls to Ra 0.4 to 0.8 micrometers. Anything rougher than Ra 1.0 micrometers will scratch soft coatings.
Polish in the direction of strip travel, not across it. Cross-direction polish marks show up as repeating stripes on the profile. Use progressively finer compounds, ending at 600 to 1200 grit, then buff to the target Ra.
Solution 2: Set the Roller Gap Below Nominal Thickness
Roller gap is the space between the upper and lower rolls at each stand. Too wide and the profile loses shape; too tight and the strip thins and scratches.
For forming passes, start at nominal material thickness minus 0.10 to 0.20 millimeters on a new tooling set. Sizing and finishing passes run at nominal minus 0.00 to 0.05 millimeters. Guide passes stay at nominal plus 0.30 to 0.50 millimeters so the strip never touches the roll faces.
Measure actual coil thickness with a micrometer before setup, not the nominal certificate value. The full method is in the roller gap clearance guide.
Solution 3: Use Chrome-Plated or Coated Rollers
Chrome plating changes how the roll surface behaves. Hard chrome at 850 to 1100 HV is about twice as hard as D2 tool steel at 58 to 62 HRC, so it resists abrasive wear longer.
Plate thickness of 20 to 30 micrometers gives the best balance. Thinner plating wears through quickly. Thicker plating chips at the edges.
For stainless steel and galvanized strip, consider PVD titanium nitride (TiN) coatings on top of chrome. TiN lowers friction to about 0.4 and reduces pick-up and galling, at 15 to 30 percent more cost than chrome alone. Coating selection guidance comes from PMA.
Solution 4: Balance Roll Pressure Across the Flower Pattern
Scratches often come from one overloaded stand, usually a breakdown pass carrying the highest load.
Check each stand for over-bending. Overload shows as edge thinning, a shiny stripe along the bend line, or exit flare. Reduce pressure and shift load to the next stand.
Correct pass design spreads the bend over 4 to 8 incremental stands instead of 1 or 2 heavy ones. If scratches appear after a die change, compare the flower pattern against the original drawings.
Solution 5: Clean the Strip and Control Lubricant Film
Dirt on the coil becomes scratches on the profile. A 10 micrometer dust particle trapped between the roll and strip is enough to score galvanized coating.
Install a strip cleaner or wiper ahead of the first stand. Brush or air-knife systems remove fines. For pre-painted coil, confirm the coating is fully cured before forming, because soft paint transfers onto the rolls and creates repeating mark defects.
Light lubrication helps on stainless and aluminum. Use a thin film of forming oil at 5 to 15 milliliters per square meter. Too much oil attracts dirt. Too little promotes galling.
Solution 6: Schedule Re-Polishing and Gap Audits
Roll surfaces wear every shift. A clean roll can start scratching after a coating change or a batch of dirty coil.
Schedule a re-polish every 2,000 to 3,000 operating hours, or every 6 months, whichever comes first. Audit فجوة الأسطوانة at the same interval with a feeler gauge or lead wire method. Check for coating pick-up after every coil change.
Track defect reports per shift. Log the stand number, coil batch, and roll face condition. That log turns random defects into a predictable maintenance trigger.

Defect Diagnosis Table
Use this table to match the defect you see to the cause and the fix.
| عيب | Typical Cause | Quick Fix |
|---|---|---|
| Continuous line scratch along strip | Rough roll face, embedded debris | Re-polish roll to Ra 0.2 to 0.4, clean rolls |
| Repeating mark every roll revolution | Coating pick-up or chip on roll | Remove pick-up, polish damaged spot |
| Edge thinning plus scuffing | Roller gap too tight at forming stand | Open gap to nominal minus 0.10 to 0.20 mm |
| Intermittent short scratches | Dirty coil, scale, or metal fines | Install strip cleaner, wipe rolls per shift |
| Heavy metal transfer, rough surface | Galling from high speed and dry contact | Chrome plate or TiN coat, add light oil film |
| White or grey haze on galvanized | Zinc dust on rolls or strip | Clean rolls, reduce speed below 60 m/min |
Roller Surface Finish Selection Table
Pick the right finish before you order new tooling. The Ra value decides how the surface behaves.
| طلب | Target Ra | Polish Method | ملحوظات |
|---|---|---|---|
| Exposed surfaces, pre-painted strip | 0.2 to 0.4 µm | Polish to 600 to 1200 grit, buff | Lowest scratch risk |
| Guide and idle rolls | 0.4 to 0.8 µm | Fine grinding, light polish | Guides without marking |
| Breakdown and forming rolls | 0.4 to 0.6 µm | Ground, polished along travel | Balance grip and surface quality |
| Hard-to-form stainless, high strength | 0.2 to 0.3 µm + chrome or TiN | Polish then plate | Prevents galling and pick-up |
| Non-contact back-up rolls | 1.6 to 3.2 µm | As-machined | Roughness acceptable here |
Verify the finish with a portable profilometer, not by eye; a polished roll looks identical to a scratched one until measured, a point MetalForming Magazine makes in its tooling guidance. الصيانة الوقائية لتشكيل اللفائف checks should include a surface finish reading on every audit.
How to Diagnose a Roll Forming Surface Scratch in 5 Steps
Follow this sequence when a scratch appears.
- Mark the defect location on the finished profile and measure its position across the profile width.
- Map that position back to the forming stand. A scratch at 30 percent of profile width usually comes from a roll face at the same relative position.
- Stop the line, lock out the power, and inspect the roll face at that spot with a magnifier. Look for grinding marks, chips, or pick-up.
- Measure the فجوة الأسطوانة at that stand with a feeler gauge. Compare it against the setup sheet.
- Fix the cause, run one test strip, and inspect before full production.
Never sand a roll face while the line is powered. Follow lockout tagout (LOTO) procedures first. Safety comes before a cleaner profile.
What Surface Defects Cost You
Surface defects cost money three ways: direct scrap, rework labor, and customer returns. A rejected panel is material you already paid for, and a cosmetic scratch can reject an entire shipment of visible products.
On pre-painted lines, a scratch through the zinc layer on galvanized steel exposes bare steel to corrosion. Under ASTM A653/A653M, the coating is the corrosion protection, and a deep scratch removes it locally, so the panel rusts from that line outward.
The math is simple: one 30 meter coil scratched at 40 percent reject rate wastes 12 meters of material plus the labor to handle it. Roller polish and gap maintenance costs a fraction of one rejected coil.